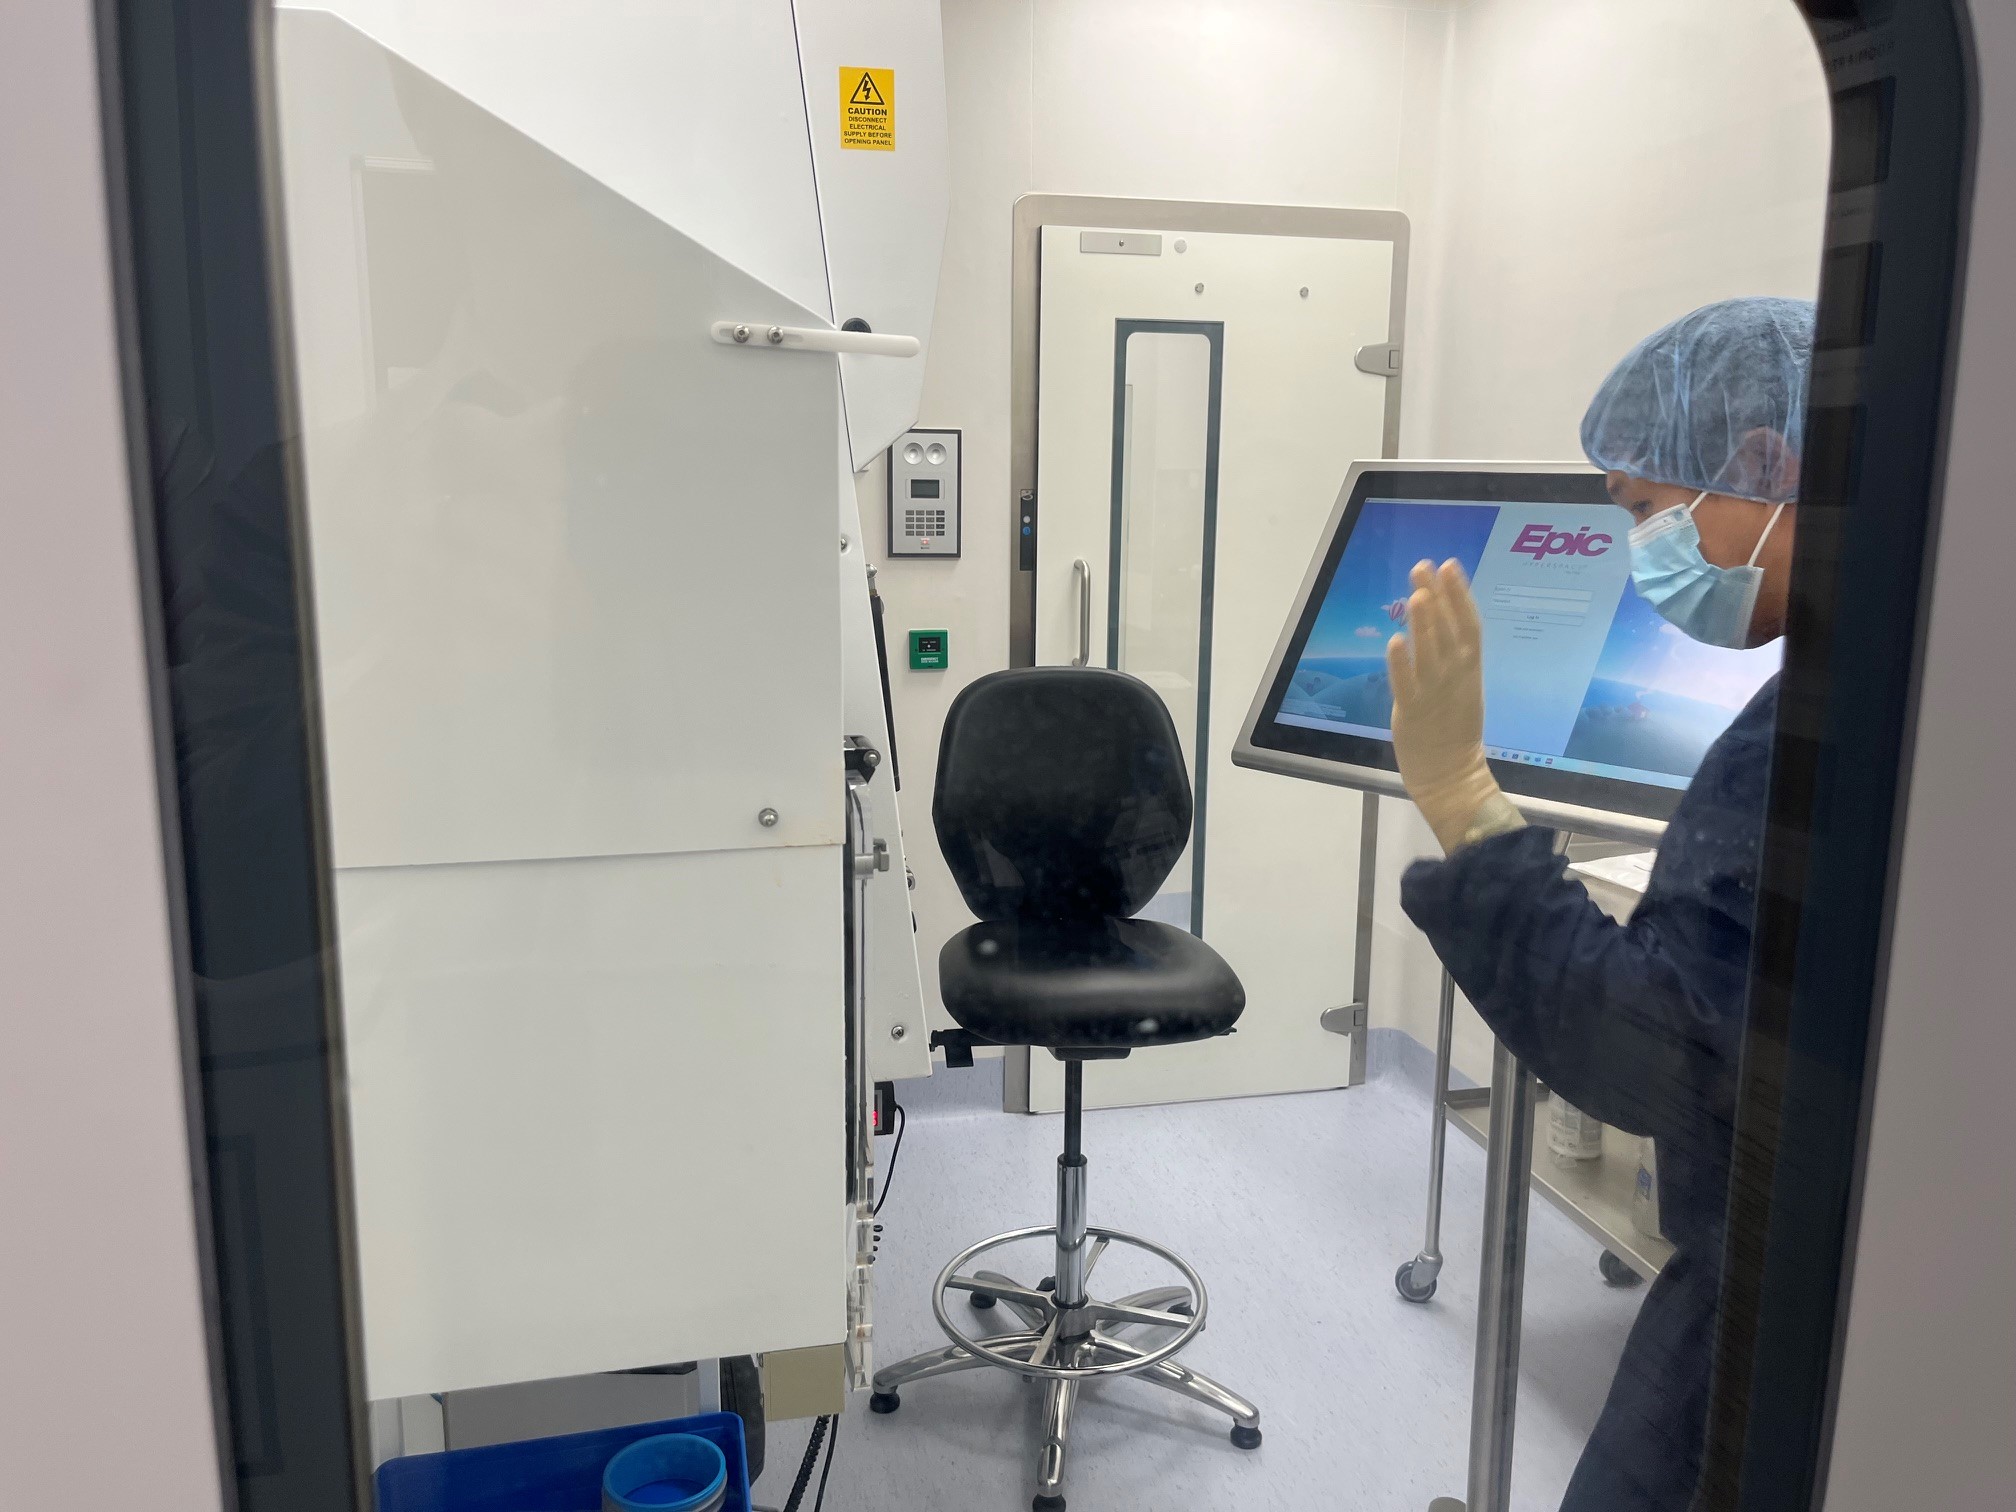
Hanley Technology has successfully supplied and installed 10 WAVE HMI Trolleys across The NHS Royal Marsden Foundation Trust’s Sutton and Chelsea sites, supporting the implementation of the new EPIC (Electronic Patient Record – EPR) software within its aseptic areas.
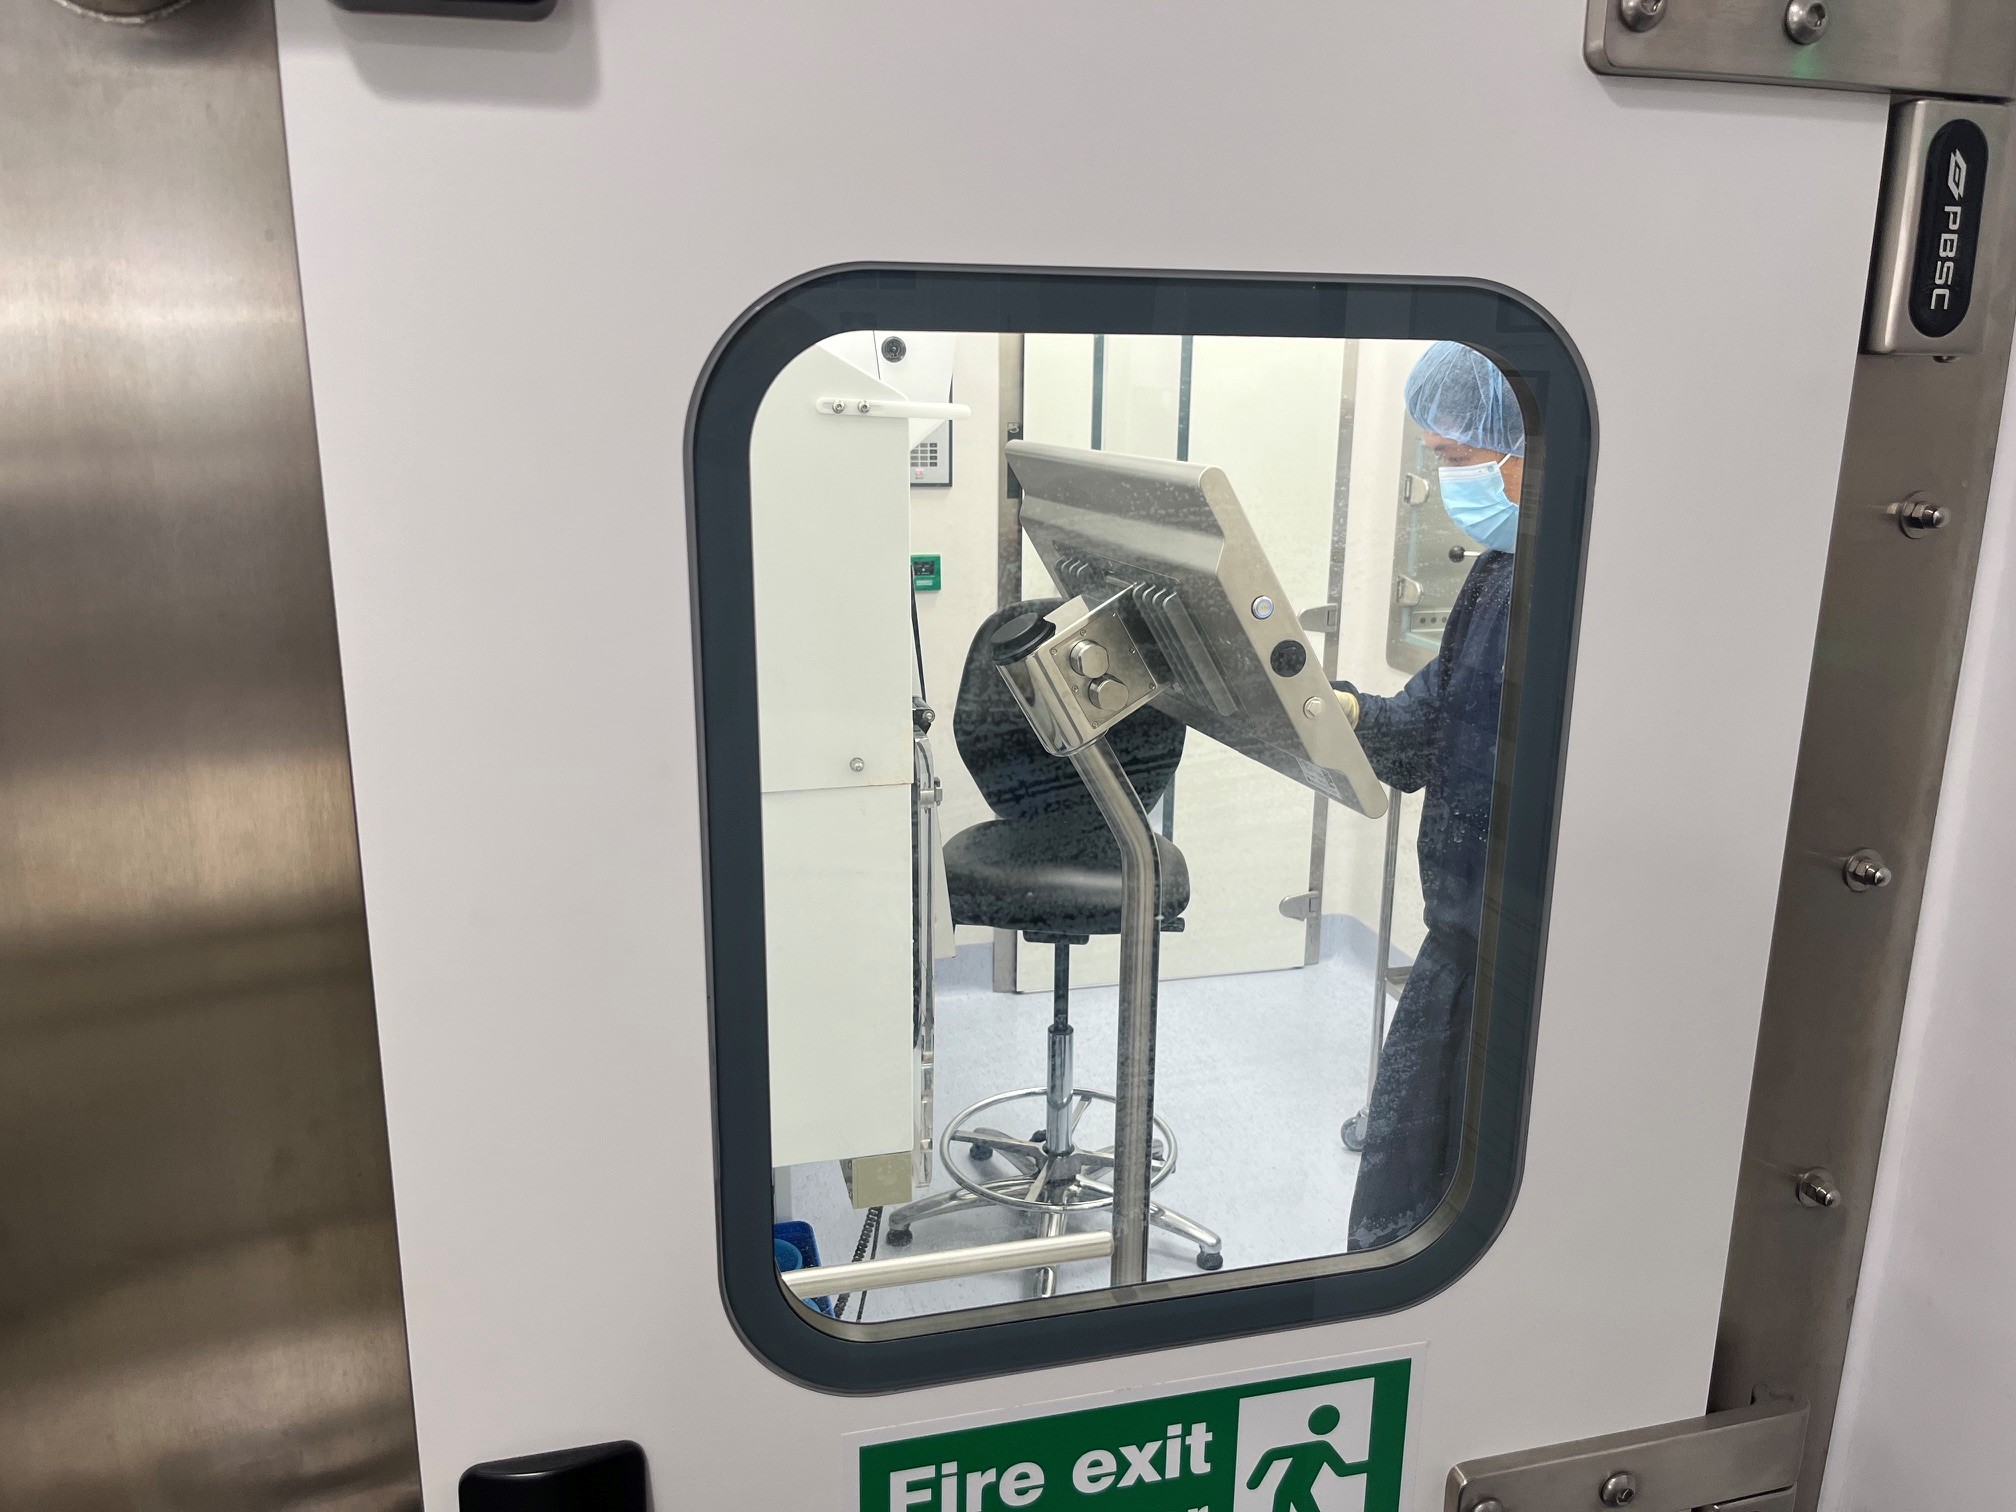
The project brings together GMP Cleanroom HMI technology, reliable Wi-Fi connectivity and full mobility around the manufacturing processes, providing operators with direct access to electronic information, data-entry functionality and flexibility throughout their workflow
The result is a more connected working environment designed to improve operational efficiency, increase data-entry accuracy, reduce downtime and minimise reliance on outdated paper-based recording systems.
This project supports the NHS’ continued adoption of digital technologies within its pharmaceutical and radiopharmacy operations, helping create a more efficient, accurate and connected working environment.
Calum Donnelly, Area Sales Manager and project lead on this delivery said:
‘It’s been a pleasure to work on a project like this directly with the NHS. Seeing the benefits they now have operationally has been incredible and I thank both of the Aseptic teams at both Sutton and Chelsea for their collaboration and hard work. To deliver such a revolutionary outcome for the site is a real success story. It won’t be long before patients start to see these benefits too!’
The Royal Marsden Foundation is a world-leading cancer trust dedicated to providing outstanding care to people affected by cancer, while also pioneering research and developing new treatments that can improve lives both in the UK and around the world. Across its Sutton and Chelsea sites, its specialist teams combine clinical expertise and cutting-edge science to keep patient care at the heart of everything they do.
Digitalisation in an Aseptic Environment
Aseptic pharmaceutical and radiopharmacy environments require equipment that can support demanding operational and cleanroom requirements while remaining practical for operators to use.
As part of its transition towards fully electronic patient records and a more modern approach to patient care, the Royal Marsden Trust required a reliable HMI workstation solution that could provide operators with access to the new EPR system directly within their harsh working cleanroom environment.
Following discussions with their project team, Hanley Technology supplied 10 24” ALLROUND WAVE HMIs, mounted on TROLLEY SLIMs, deployed across the Royal Marsden’s Sutton and Chelsea sites.
During the consultation process, testing of a demo was undertaken and the suitability of the 24” IPS LCD display (FULL HD) was confirmed. It allowed operators full interaction with the EPR and gave excellent visuals for SOPs and other information required from all around the aseptic area.
The ALLROUND variant of the WAVE HMI contains an Intel Core i5 CPU with 256GB SSD and 16GB DDR. This delivers the ability to run the EPIC software from each device individually with ample space and power to add in future applications as they transition towards fully digital processes.
The integrated Wi-Fi capability allows the HMI workstations to connect to the required network infrastructure without restricting operators to fixed workstation locations or the need for cumbersome cabling.
Rather than requiring operators to move between their work area and a fixed computer terminal, the mobile WAVE HMI Trolleys provides a workstation that can be positioned where and when it is required.
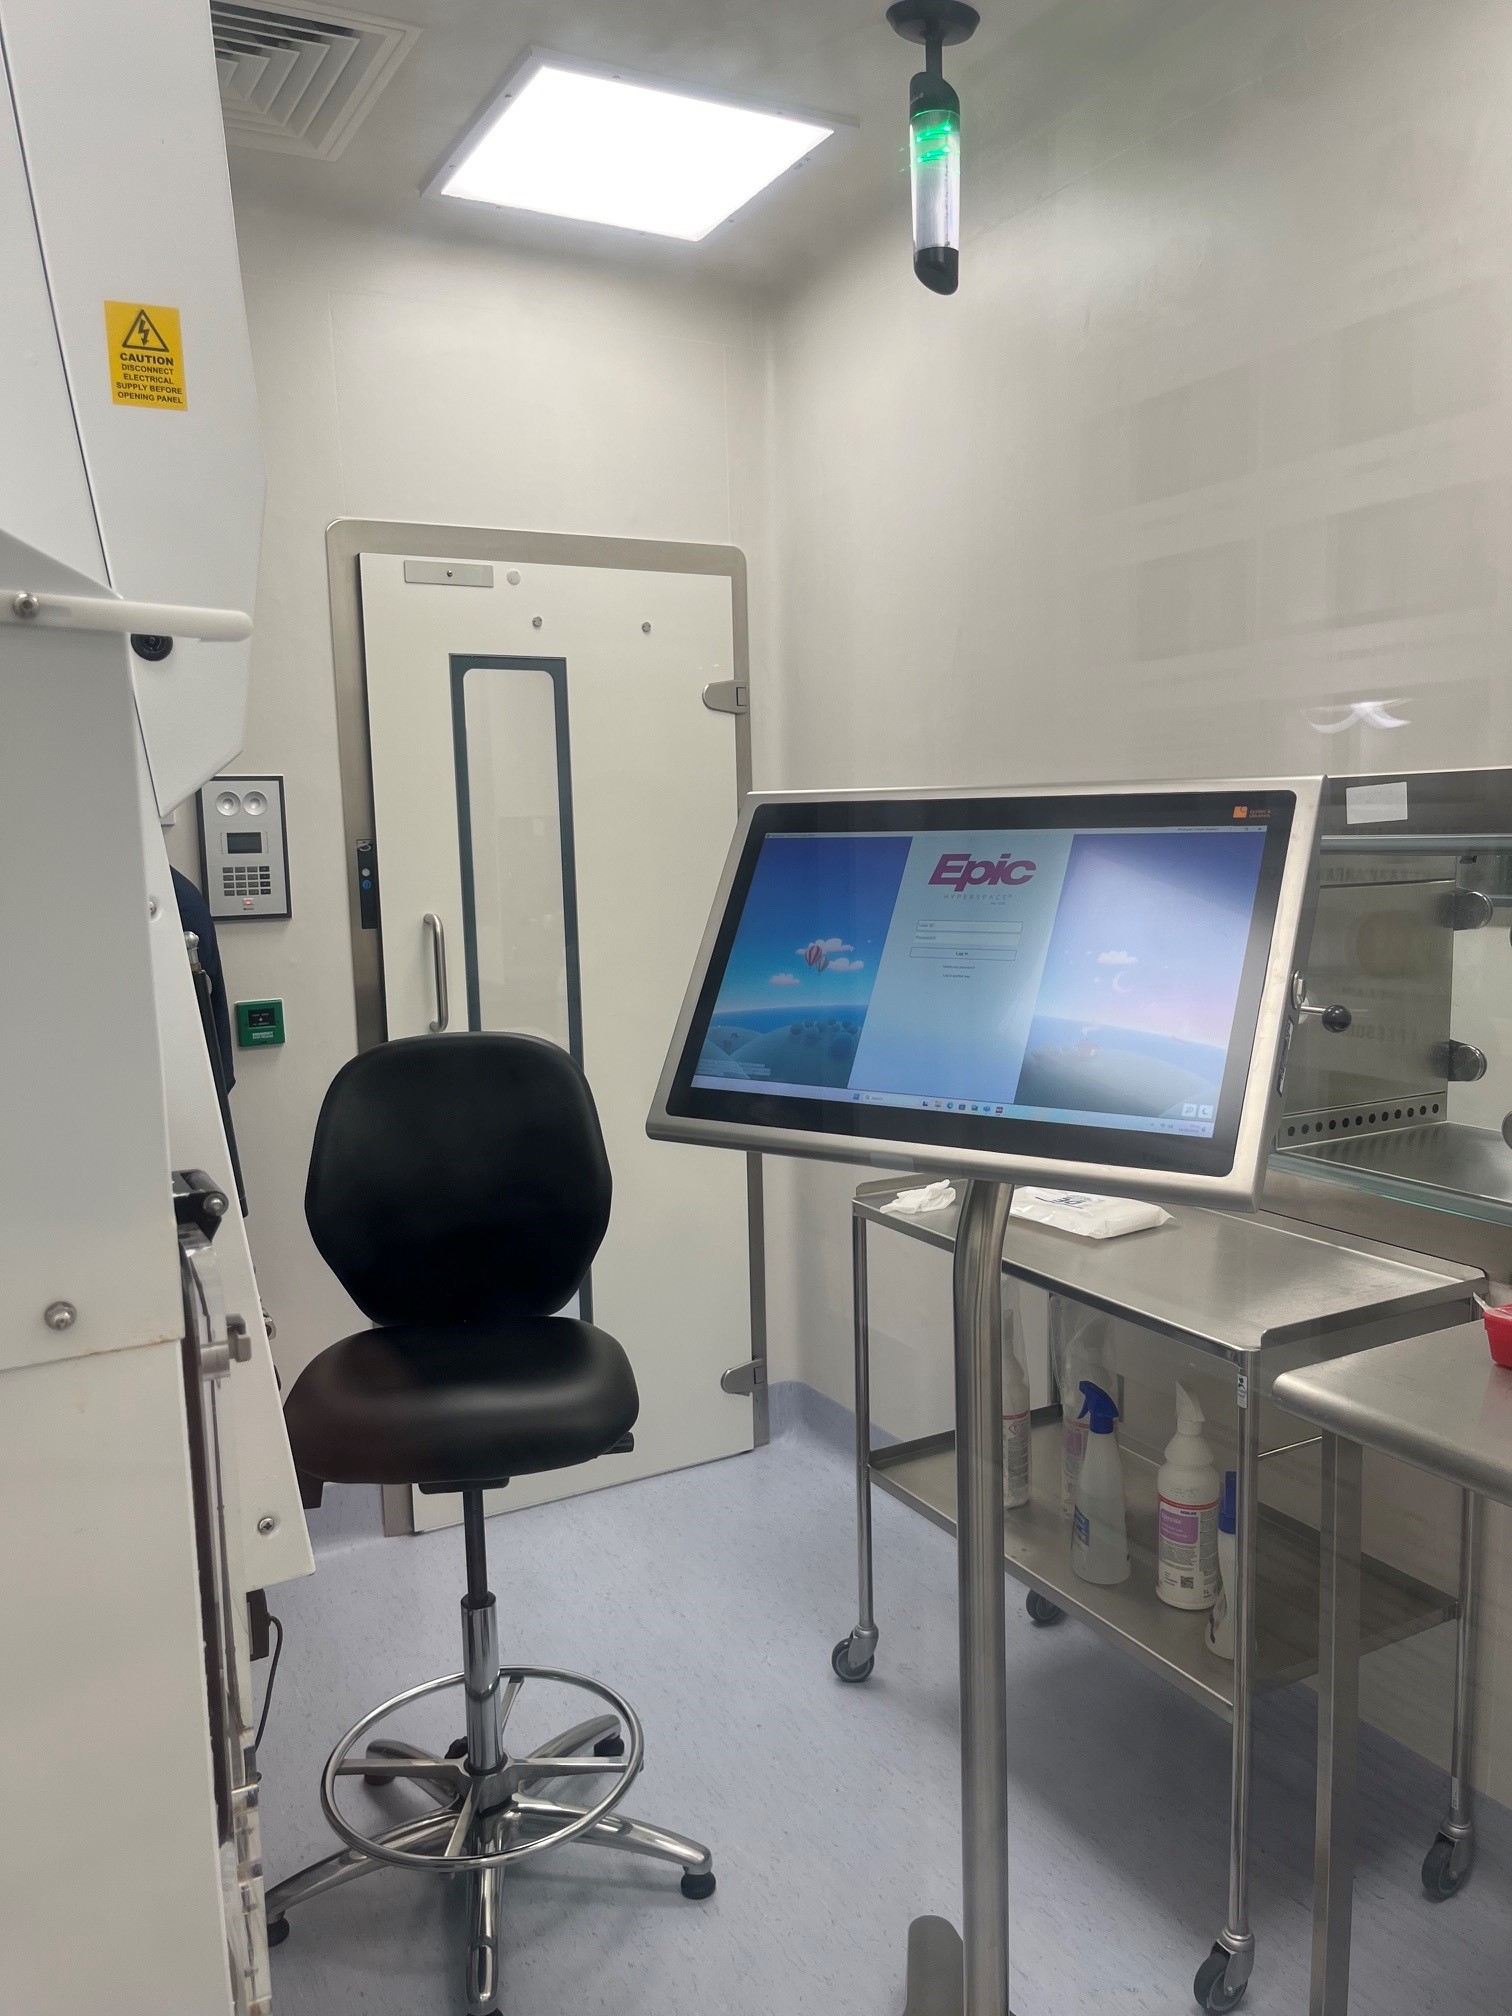
The Royal Marsden’s new EPR approach, supports the wider move towards paperless pharmaceutical manufacturing, minimising the need for operators to rely on paper records or separate recording devices. Instead, critical information can be accessed and entered electronically through the HMI.
This Royal Marsden project demonstrates how HMI hardware plays a critical role in the successful implementation of electronic patient records.
The software is only one part of a digital manufacturing system. Operators also require suitable, reliable hardware that allows them to interact with digital systems within their actual working environment.
From mobile HMI trolleys and cleanroom HMIs to GMP tablets and digital workplace solutions, Hanley Technology works with customers from across Pharmaceuticals, Life Science and Healthcare sectors to integrate reliable digital technology into critical manufacturing processes.
Whether implementing an Electronic Batch Record (EBR), Manufacturing Execution System (MES), digital work instructions or other pharmaceutical digitalisation projects, selecting the right operator interface is essential.
Talk to our experts today and discover how to modernise your Digital processes!